1. Why Aluminothermic Rail Welding Still Matters
Aluminothermic rail welding joins two rail ends with a self-contained chemical reaction. It needs no power grid, no welding machine and no heavy mobilization.
That independence is why aluminothermic rail welding remains the standard method for continuous welded rail in remote locations, for crane runways and for repairs where a mobile flash butt machine cannot reach.
This guide covers what aluminothermic rail welding is, how the reaction works, which standards govern it, and how to avoid the defects that cause most joint failures.

2. The Chemistry Behind Aluminothermic Rail Welding
The core reaction is a classic thermite reduction. Aluminium powder reduces iron oxide, releasing iron and a large amount of heat:
Fe2O3 + 2Al → 2Fe + Al2O3 + heat
The reaction temperature exceeds 2,500°C, far above the melting point of steel. The molten iron fills the mould cavity and fuses the two rail ends.
Aluminium oxide forms a lower-density slag that floats to the top of the crucible and the mould. This slag layer shields the molten steel from oxidation and must be kept out of the weld.
Formulations are not universal. Alloying additions such as carbon, manganese, vanadium and chromium are adjusted so the weld metal matches the parent rail grade — standard carbon rail, head-hardened R350HT, or a DIN 536 crane rail.
Never mix consumables from different suppliers or different formulations. Aluminothermic rail welding depends on a matched mould, crucible and charge.
3. International Standards for Aluminothermic Rail Welding
Five key references cover most aluminothermic rail welding work worldwide. Only EN 14730 and ISO 23300 are published standards; AREMA and AWS D15.2 are industry practices.
- EN 14730-1: European standard for approval of welding processes, including procedure validation.
- EN 14730-2: qualification of aluminothermic welders, approval of contractors and acceptance of finished welds.
- ISO 23300-1:2021 and ISO 23300-2:2025: the international rail welding series, covering general requirements and test methods, and aluminothermic welding specifically.
- AREMA Chapter 4 (Rail): the North American industry manual for freight, mining and heavy-haul track. Note this is an engineering practice manual, not a published standard.
- AWS D15.2: recommended practices for welding rails and related rail components. Note that AWS D15.1 covers cars and locomotives, not track.
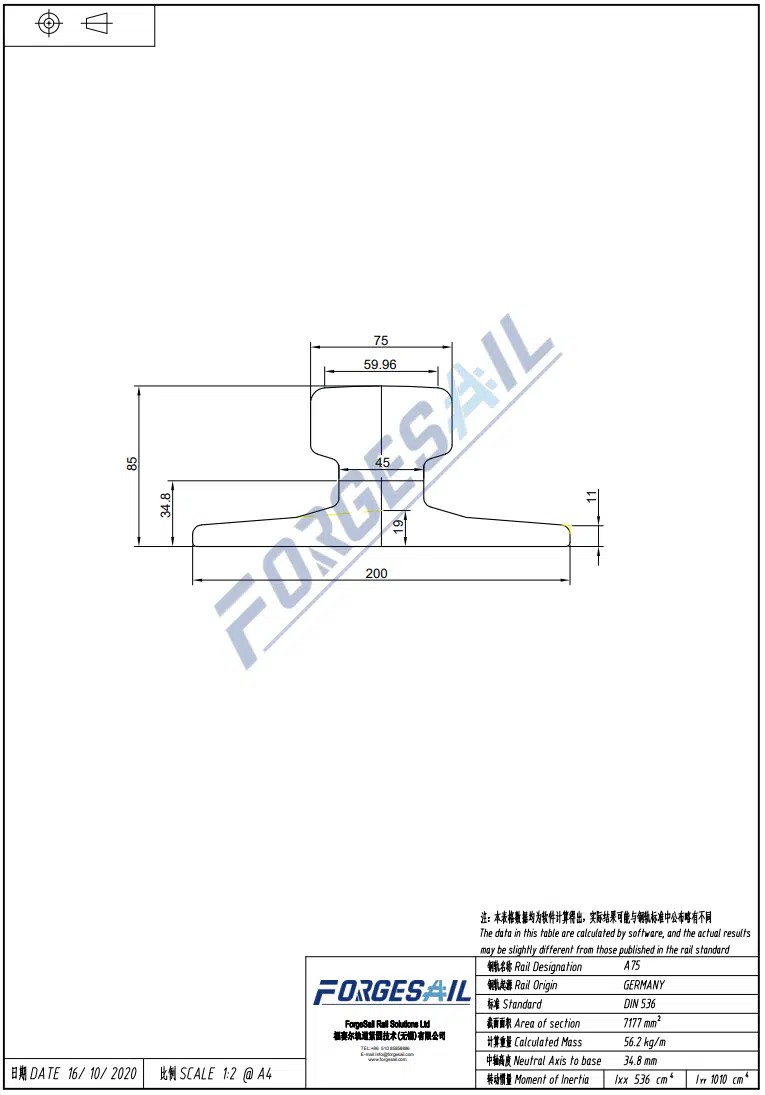
Crane rail profiles are a separate case. A-section crane rails are dimensioned to DIN 536-1 (A45–A150). This is a long-standing reference standard with no direct EN replacement for A-section crane rails, so confirm the edition specified in your project. See our guide to crane rail types for the full profile comparison.See our guide to crane rail types for the full profile comparison.
Whatever the region, the controlling document is the approved WPS (welding procedure specification), supported by the WPQR (welding procedure qualification record). Where this article gives a typical value, the WPS takes precedence.
4. Field Execution: 6 Steps of Aluminothermic Rail Welding
Field quality depends on six steps. Skipping or rushing any one of them is the root cause of most failures.
Step 1: Joint alignment and gap setting
Align the rail ends and set the gap specified in the welding procedure. Gap values are kit-specific and vary with rail section and ambient temperature — many processes sit near 25 mm, while some run 30–35 mm. Never assume a universal value.
Preset the vertical crown so the finished weld compensates for cooling shrinkage. Confirm alignment with a straight edge before clamping.
Step 2: Mould clamping and sealing
Fit the refractory mould and seal every joint with sealing paste or sand. A poor seal allows molten steel to escape as a run-out, which ruins the joint and creates a safety hazard.

Step 3: Uniform preheating
Preheat both rail ends with a controlled burner to the temperature stated in the procedure — commonly 900–1,000°C on the rail head. Even preheat prevents lack of fusion. On head-hardened grades such as R350HT, watch the upper limit: excessive preheat causes decarburisation and local hardness loss.
Cold weather changes the preheat and cooling window. Our guide to thermite welding weather conditions covers the field limits in detail.

Step 4: Crucible ignition and self-tapping
Ignite the charge in the crucible. The automatic thimble holds the molten steel until the reaction completes, then releases it into the mould. This delay lets the slag separate before pouring.

Step 5: Demetalling and shearing
Remove the mould and shear off the excess weld collar at the time specified in the procedure. Too early and the weld is still soft; too late and the material is too hard to shear cleanly.
Step 6: Profile grinding and testing
Grind the weld to restore the rail head running profile within the tolerance specified by the standard, then cool fully and inspect. Ultrasonic testing (UT) is used to confirm internal soundness before the joint is accepted.
For a detailed fault list and causes, see thermite welding defects prevention.

5. Aluminothermic vs Flash Butt vs Enclosed Arc Welding
The table below compares the three main rail joining methods. For a deeper head-to-head on the two most common options, read flash butt vs thermite welding.
| Factor | Aluminothermic (ATW) | Flash Butt (FBW) | Enclosed Arc (EAW) |
| Capital cost | Low | Very high | Low to moderate |
| Mobilization | Fully portable, no power needed | Heavy machine, generator, crane | Moderate, needs power |
| Cycle time per joint | Longer (mould, preheat, cooling) | Short once set up | Moderate |
| Joint quality | Cast structure; lower fatigue performance than FBW | Forged structure; highest fatigue performance | Good for repair work |
| Heat-affected zone | Wider, cast structure | Narrow, forged structure | Narrow to medium |
| Confined / elevated access | Excellent | Poor | Fair |
| Best suited to | Crane rails, repairs, turnouts, remote sites | Long mainline CWR campaigns | Specific repairs and closures |
6. Safety and Working Conditions
Aluminothermic rail welding is a high-temperature, high-risk operation. The reaction cannot be stopped once ignited.
Moisture is the single biggest hazard. Water contacting molten steel flashes to steam and can eject molten metal. Never weld in rain, snow or fog, or on a wet rail seat — these limits are covered in our weather conditions for thermite welding guide.
Keep the working area dry and clear. Use a hot work permit, fire watch and appropriate PPE including a face shield, heat-resistant gloves and flame-retardant clothing.
Provide ventilation in tunnels and enclosed spaces. The reaction produces fumes and dust that must be extracted.
If rain starts before ignition, stop and protect the equipment. If the reaction has already started, withdraw all personnel to a safe distance and never attempt to cover the mould.
Transport classification matters too. Aluminothermic charges contain aluminium powder, and the aluminium powder component is classified as a water-reactive dangerous good (Class 4.3). Charges must be shipped and stored under the applicable UN classification and packing group stated on the supplier’s safety data sheet (SDS) — confirm the exact UN number with your supplier and freight forwarder before sea or road shipment.
7. Common Defects and How to Prevent Them
Most aluminothermic rail welding defects trace back to moisture, contamination or timing. It also helps to remember that an aluminothermic weld is a cast structure, not a forged one — this is what sets its fatigue behaviour apart from flash butt welds. We cover the full fault library in thermite welding defects and prevention; the four most common are summarised here.thermite welding defects and prevention
Gas porosity
Round voids inside the weld, caused by moisture in the consumables, a wet mould, or a damp rail surface. Keep consumables sealed and preheat correctly.
Slag inclusion
Slag trapped inside the weld, caused by pouring before the reaction completes or by a poorly sealed mould. Use an automatic thimble and check the seal.
Lack of fusion
The rail ends are not fully melted, caused by low preheat, a gap that is too small, or contaminated rail ends. Clean the ends and follow the preheat procedure.
Hot cracking
Transverse cracks that form while the weld is still hot, caused by premature demoulding, early shearing or rapid cooling. Respect the cooling and demoulding times.
All four are prevented by the same discipline: a matched consumable set, a dry site, controlled preheat, and correct timing.
8. Consumable Storage and Shelf Life
Aluminothermic rail welding consumables are moisture-sensitive. Storage directly affects weld quality — and charge selection drives cost.
- Keep charges, moulds and crucibles sealed in their original packaging until use.
- Store in a dry, ventilated area away from damp floors and open water.
- Use first-in, first-out stock rotation and check the expiry date on every batch.
- Protect moulds and crucibles from impact and deformation; a damaged mould will not seal.
- Record the batch number of every joint so quality issues can be traced back.
- Critical: a charge that has been exposed to moisture cannot be dried and reused. Damp charge must be withdrawn and scrapped as a whole batch — a wet charge risks incomplete reaction, weld defects and, in storage, spontaneous ignition.
9. Heavy-Load Industrial Applications
Aluminothermic rail welding is widely used where loads are high and access is difficult.
Container terminals and port cranes
STS and ASC crane runways take repeated dynamic impact. The load path through rail, rail pads and crane rails is analysed in our crane rail force analysis article.
Mining and heavy haul
Heavy-haul lines with axle loads above 30 tonnes demand tight gap control and consistent preheat to avoid joint batter.
Overhead factory cranes
In-situ jointing on roof trusses or elevated girders is often impossible with a mobile flash butt machine. Aluminothermic rail welding remains the practical option. Track stability also depends on the base, so see rail foundation grouting for installation requirements.
10. Project Experience
ForgeSail has supplied aluminothermic welding kits and on-site technical support on heavy industrial rail projects, including the King Salman International Complex for Marine Industries and Services in Saudi Arabia, where A45 to A150 crane rails were installed with full fastening systems and 6,597 aluminothermic welds completed.
This field experience shapes how we specify consumables: matched to the rail grade, the local climate and the client’s welding procedure.

11. FAQ
Is aluminothermic rail welding as strong as flash butt welding?
Not in fatigue terms, which is what matters most on rail. Flash butt welding produces a forged structure, while an aluminothermic weld is cast; this gives flash butt better fatigue performance and a narrower heat-affected zone. Aluminothermic welding is still widely used for continuous welded rail where the process is approved, controlled and correctly specified.
What temperature does the reaction reach?
The thermite reaction exceeds 2,500°C, well above the melting point of steel.
Can aluminothermic rail welding be used on crane rails?
Yes. It is widely used on crane runways and elevated girders where a mobile flash butt machine cannot reach.
What rail gap should be used?
Gaps are kit-specific. Many processes use around 25 mm, but some run 30–35 mm depending on the consumable set, rail section and temperature. Always follow the supplier’s procedure.
Can aluminothermic rail welding be done in the rain?
No. Moisture causes steam explosions and weld defects. Never weld in rain, snow or fog.
How long does one joint take?
The weld itself is fast, but the full cycle includes mould assembly, preheat, pouring, cooling and shearing. Plan the whole cycle, not just the pour.