




Thermite (Aluminothermic) Welding Kits for Crane & Railway Rail

Thermite Welding Consumables/Materials; Aluminothermic Welding Kits
Our ForgeSail thermite welding kits are professional rail connection tools, also known as aluminothermic welding kits, widely used for crane rail, turnout and railway track field welding. Thermite welding flux is a specialized material used in aluminothermic (thermite) welding. It leverages the intense exothermic reaction between aluminum and oxygen at high temperatures to generate extreme heat, melting metal into molten steel and enabling the permanent welding of metallic components, such as rails.
What Are Aluminothermic Welding Kits
Aluminothermic welding kits are complete systems designed for on-site rail welding, utilizing the exothermic reaction between aluminum powder and iron oxide to produce molten steel at temperatures exceeding 2,500°C. ForgeSail’s aluminothermic welding kits include all necessary components—thermite welding portion, sand mould, one-shot crucible, and accessories—for seamless rail joint welding. Our aluminothermic welding kits are widely used in railway construction, crane rail installation, metro lines, and industrial track maintenance.
Included Components
Thermite Welding Portion

A specialized material for aluminothermic (thermite) welding, generating extreme heat to melt metal and permanently weld rails and other metallic components.
Applications:
Continuous welded rail (CWR) joints for railways
Seamless welding of crane rails, metro and tram lines, and industrial tracks
Key Components:
Iron oxide powder: Main reactant
Aluminum powder: Fuel for exothermic reaction
Alloy additives: Enhance weld properties (e.g., ferrosteel, ferromanganese, ferrovanadium)
Features & Advantages:
Produces molten steel and slag >2,500°C for strong, durable welds
Portable and easy to operate in field conditions
High welding efficiency
Safety & Handling:
Maintain precise component ratios
Store in dry, ventilated conditions
Use heat-resistant gloves, goggles, and protective clothing
Follow strict ignition protocols
Sand Mould for Thermite Welding

A high-temperature vessel made from compressed quartz sand, designed for thermite welding of continuous welded rails (CWR).
Functions:
Reaction Chamber: Hosts the exothermic thermite reaction
Self-Pouring: Automatically releases molten steel into the sand mould
Key Features:
Quartz sand body withstands >2,500°C; iron casing protects against moisture and impact
Compatible with standard rail profiles (UIC, AREMA, DIN)
Applications:
Railway, metro, and tram CWR joints
Crane rails in steel mills, ports, shipyards, and industrial facilities
Notes:
Single-use for consistent reaction and safety
Store in original packaging to keep dry
One-Shot Crucible for Thermite Welding

A high-temperature vessel made from compressed quartz sand, designed for thermite welding of continuous welded rails (CWR).
Functions:
Reaction Chamber: Hosts the exothermic thermite reaction
Self-Pouring: Automatically releases molten steel into the sand mould
Key Features:
Quartz sand body withstands >2,500°C; iron casing protects against moisture and impact
Compatible with standard rail profiles (UIC, AREMA, DIN)
Applications:
Railway, metro, and tram CWR joints
Crane rails in steel mills, ports, shipyards, and industrial facilities
Notes:
Single-use for consistent reaction and safety
Store in original packaging to keep dry
Thermite Welding Flux Specifications
| Item | Specification Details |
|---|---|
| Product Series | Tie IIIDE Series, QU Series, A Series |
| Application | Suitable for U75V material; also applicable for welding of U71Mn and U76NbRE rails. |
| Adopted Process | Thermite welding process using Tie IIIDE series, QU series, and A series thermite fluxes. |
| Casting Method | One-time crucible self-melting, side-top pouring. |
| Reserved Rail Gap | 26 ± 2 mm |
| Weld Hardness | Hot-rolled rail: Base Metal ± 20 HBW |
| Tensile Strength | 880MPa grade rail: Rm ≥ 710 MPa 980MPa grade rail: Rm ≥ 780 MPa |
Superior Electrical & Mechanical Integrity
- Seamless Conductivity: The welded joint provides current interception identical to the original wire, ensuring zero power loss.
- High Surge Tolerance: Engineered to withstand repeated, massive surge (fault) currents without any molecular degradation.
- Exceptional Strength: The resulting solder joint bonds at a molecular level, proving physically tougher than copper itself..
Superior Electrical & Mechanical Integrity
- 100% Self-Contained: Requires absolutely no external power, batteries, or heat sources to operate.
- Ultra-Portable & Easy to Use: Lightweight and simple to operate, dramatically reducing labor costs and installation time in remote areas.
- Instant Quality Assurance: Welding quality can be easily and quickly verified through a simple visual inspection.
Superior Electrical & Mechanical Integrity
- Permanent Connection: Creates a lifelong bond that will never suffer from high resistance caused by mechanical looseness or aging.
- Corrosion-Proof: Highly impervious to harsh corrosives, making it the ultimate zero-maintenance solution for underground or exposed environments.
Superior Electrical & Mechanical Integrity
- Broad Application: Capable of permanently fusing a wide variety of metals, including pure copper, copper alloys, copper-plated steel, stainless steel, and high-resistance heating materials.
Welding Process Parameters with Thermite
| Rail Profile | Oxygen Pressure (MPa) | LPG Pressure (MPa) | Flame Core Length (mm) | Preheat Time (min) | Oxygen Flow (L/h) | Reserved Rail Gap (mm) |
|---|---|---|---|---|---|---|
| 18kg - 24kg | 0.4 | 0.07 | 15 - 20 | 3 | 3500 | 26 ± 2 |
| 38kg - 43kg | 0.4 | 0.07 | 15 - 20 | 4 | 3500 | 26 ± 2 |
| 50kg | 0.4 | 0.07 | 15 - 20 | 4 | 3500 | 26 ± 2 |
| 60kg | 0.4 | 0.07 | 15 - 20 | 5 | 3500 | 26 ± 2 |
| A55 | 0.4 | 0.07 | 15 - 20 | 4 | 3500 | 26 ± 2 |
| A65 | 0.4 | 0.07 | 15 - 20 | 4.5 | 3500 | 26 ± 2 |
| A75 | 0.4 | 0.07 | 15 - 20 | 5 | 3500 | 26 ± 2 |
| A100 | 0.4 | 0.07 | 15 - 20 | 9 | 3500 | 26 ± 2 |
| A120 - A150 | 0.4 | 0.07 | 15 - 20 | 15 | 3500 | 26 ± 2 |
| QU70 - QU80 | 0.4 | 0.07 | 15 - 20 | 5 | 3500 | 26 ± 2 |
| QU100 | 0.4 | 0.07 | 15 - 20 | 9 | 3500 | 26 ± 2 |
| QU120 | 0.4 | 0.07 | 15 - 20 | 12 | 3500 | 26 ± 2 |
Need proper execution guidelines for your site engineers?
DOWNLOAD THERMITE WELDING OPERATION GUIDE (PDF)* Includes safety protocols, crucible setup, and post-weld grinding instructions.
FAQs
Q: What are aluminothermic welding kits used for?
Aluminothermic welding kits are complete rail joining systems that use the exothermic reaction between aluminum powder and iron oxide to produce molten steel at over 2,500°C. These aluminothermic welding kits are primarily used for:
- Continuous welded rail (CWR) joints in railway construction
- Crane rail welding in steel mills, ports, and shipyards
- Metro and tram line track installation
- Industrial track maintenance and repair
ForgeSail's aluminothermic welding kits are designed for field use — no external power required, portable, and capable of delivering strong, permanent welds in under 30 minutes per joint.
Q: What components are included in a complete aluminothermic welding kit?
A standard ForgeSail aluminothermic welding kit includes 6 essential components:
- Thermite welding portion — pre-measured flux powder (iron oxide + aluminum + alloy additives) for the exothermic reaction
- Sand mould — high-temperature quartz sand mould that shapes the weld joint
- One-shot crucible — reaction vessel that holds the thermite charge and automatically pours molten steel
- Ignition powder — for safe, reliable ignition of the thermite reaction
- Sealing sand — prevents molten steel leakage during welding
- Disc gate — a ceramic disc that seals the crucible bottom until the reaction is complete
Optional accessories include gap retainers, mould clamps, and preheating torches. Everything you need for on-site rail welding comes in one complete aluminothermic welding kit.
Q: Can aluminothermic welding kits be used for crane rail welding?
Yes. ForgeSail aluminothermic welding kits are specifically engineered for both railroad track and crane rail applications. Crane rail welding requires higher precision because crane rails often handle heavier point loads and operate in harsh environments like steel mills, ports, and mining facilities.
Our aluminothermic welding kits for crane rails feature:
- Custom-formulated flux for high-hardness rail profiles
- Sand moulds compatible with A150, A100, A75, and other crane rail profiles
- Optimized weld cycles that minimize heat-affected zone (HAZ) width
- Proven in over 800 crane rail projects across 15+ countries
Q: How long does the aluminothermic welding process take?
A complete aluminothermic welding cycle takes approximately 25-35 minutes per joint, broken down as follows:
| Step | Time |
|---|---|
| Mould assembly and alignment | 5 min |
| Preheating the mould | 3-5 min |
| Crucible setup and ignition | 2 min |
| Thermite reaction and pouring | 30-60 sec |
| Cooling time | 10-15 min |
| Mould removal and inspection | 3-5 min |
The actual exothermic reaction itself is over in under a minute — once ignited, it reaches over 2,500°C in seconds. ForgeSail aluminothermic welding kits are designed for fast, reliable field operation with minimal downtime.
Q: What is the difference between aluminothermic welding and flash butt welding?
The main difference between aluminothermic welding and flash butt welding lies in the equipment, portability, and application:
Aluminothermic welding:
- Uses a chemical reaction (thermite) to generate heat — no external power source needed
- Portable equipment — ideal for field and remote site welding
- Lower upfront equipment cost
- Suitable for both crane rail and railway track, especially in tight spaces
- Weld cycle: ~30 minutes per joint
Flash butt welding:
- Uses electrical resistance to generate heat
- Requires a stationary welding machine and power supply
- Higher initial investment but faster per-joint speed for mass production
- Primarily used in factory continuous welding or long-distance rail laying
For most on-site rail construction, maintenance, and crane rail projects, aluminothermic welding kits offer the best balance of portability, cost, and weld quality.
Read more: Flash Butt vs Thermite Welding: 7 Key Differences You Must Know
Q: Which rail profiles are compatible with your aluminothermic welding kits?
ForgeSail aluminothermic welding kits support a wide range of rail profiles, including:
- UIC standards: UIC 60, UIC 54, UIC 50
- AREMA standards: 115RE, 132RE, 136RE
- DIN standards: DIN 60, DIN 54
- Crane rail profiles: A150, A120, A100, A75, A65, QU100, QU80
- GB (Chinese) standards: 60kg/m, 50kg/m, 43kg/m
- Other:Custom moulds available for special profiles
Our standard aluminothermic welding kits cover 85% of common rail profiles, and we offer custom sand moulds and flux formulations for special applications.
Q: How are aluminothermic welding kits packaged and shipped?
ForgeSail packages aluminothermic welding kits for safe international shipping:
- Standard packaging: 4 kits per sealed box, 4 boxes per pallet (16 kits per pallet)
- Each thermite welding portion is individually vacuum-sealed to protect against moisture
- Sand moulds are individually wrapped with foam padding to prevent damage
- Kits are packed in export-grade plywood crates or carton pallets
- Lead time: 15-25 working days for standard kits; 25-35 for custom formulations
- Shipping: FOB Shanghai / CIF available for global delivery
Moisture protection is critical — our packaging ensures the thermite flux stays dry during ocean freight and on-site storage.
Reference Projects


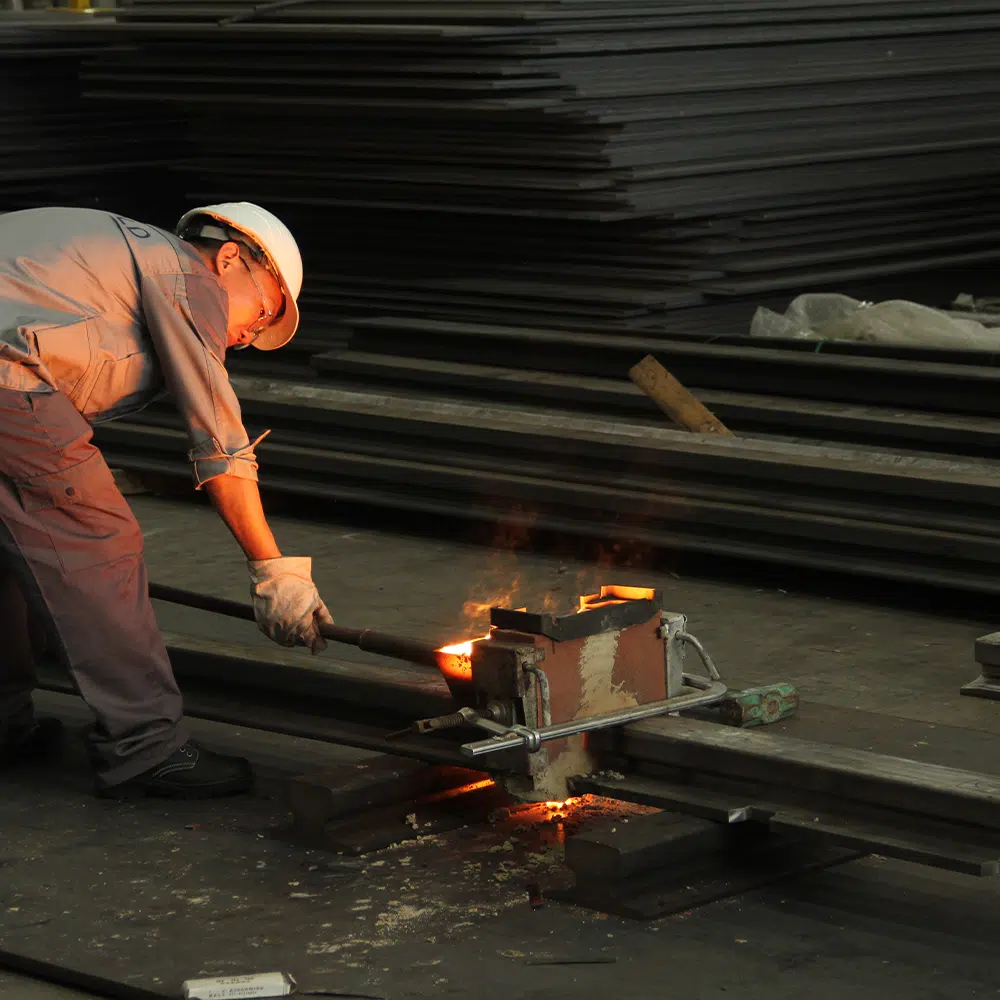
Why Choose Our Aluminothermic Welding Kits?
8 Key Advantages of Our Thermite Welding Kits:
- Complete all-in-one kit — ready for field use
- Suitable for 24-120 kg/m rail profiles (UIC, AREMA, DIN, GB)
- Welding temperature >2,500°C for deep fusion
- Simple operation with pre-measured flux portions
- Quick weld cycle — under 30 minutes per joint
- Portable equipment — no external power needed
- Proven in 3,500+ projects across 15+ countries
- Custom formulations for crane rail, tram, and high-speed rail
