Forgesail Engineering & Technical Team | 2026-08
Core Viewpoint: The rubber nose is a structural functional component designed to withstand cyclic uplift forces. Flexible rail clips with rubber noses outperform rigid ones in 7 of 11 engineering comparison dimensions and are the de facto global standard for crane rail fasteners. Related: FORGESAIL Crane Rail Clips
However, industry consensus acknowledges the trade-off: rubber noses age, wear down, and cannot be replaced independently under traditional architectures. Forgesail addresses this industry pain point through three strategic tiers:
- Optimize nose design, materials, and production processes to improve the quality of mainstream products.
- Rely on China-based in-house manufacturing facilities to support customized noseless solutions for rare special operating conditions.
- Use a wrap-around (encapsulated) replaceable rubber nose (patent application submitted) to turn the rubber nose from a disposable component into an independently replaceable standard wearing part.
1. Understanding the “Bow Wave” First — The Fundamental Reason for the Rubber Nose
A crane rail clip rubber nose is the elastomer component that applies preload to the rail foot and absorbs bow-wave uplift. It is also called an elastomer nose or elastomeric nose.
In structural mechanics, when a rail is laid on elastic pads and steel/concrete beams, it essentially acts as a continuous beam on an elastic foundation. When a heavy-duty crane wheel (with individual wheel loads reaching 300–500 kN) moves along the rail, the rail beneath the wheel bends downward. Simultaneously, the rail sections immediately adjacent to the front and rear of the wheel are lifted upward due to the reverse action of bending moments. This vertical rail deflection waveform moving synchronously with the wheel is known in crane engineering as the “bow wave”, a classic mechanical response of a beam on an elastic foundation under a moving concentrated load. Systematically expounded by Hetényi (1946) in Beams on Elastic Foundation, this is foundational knowledge in structural mechanics and not proprietary to any single vendor.

Figure 1: Bow Wave Phenomenon — Vertical deflection waveform of a beam on an elastic foundation under a moving concentrated force; the rubber nose bears not static pressure but cyclic uplift force
| Diagram Component | English Description |
| Wheel Load | Crane Wheel · Heavy Wheel Load (300-500 kN) |
| Deformation Wave | Rail Deflection (Exaggerated Deformation Schematic) |
| Uplift Points | Uplift Force ↑ at adjacent front/rear locations of the wheel |
| Nose Component | Red = Rubber Nose (Absorbs cyclic uplift displacement) |
| Support Base | Crane Girder / Steel Sole Plate & Elastic Rail Pad |
The engineering consequences of bow waves are repeatedly validated by international and national standards and field practice: rail clip bolts undergo high-frequency alternating tensile loads rather than simple vertical toe loads. The American Institute of Steel Construction (AISC) explicitly notes in New Fatigue Provisions for the Design of Crane Runway Girders that the twisting-camming action of single-bolt clips caused by longitudinal rail creep continually forces the rail out of alignment. Domestic engineering literature (Improvement of General Overhead Crane Rail Clips) records a field failure chain involving a 50 kg/m rail and 740 clips: bow wave rebound forces, nut loosening, clip displacement, rubber nose detachment, and rail uplifting by 20-30 mm. Clip loosening and migration caused by uplift forces represent the most common failure mode in rail fastener systems. The rubber nose is the functional component engineered to absorb this uplift force. Also read: Crane Rail Clip Types Comparison
2. Four Core Functions of the Rubber Nose
In a typical flexible rail clip assembly (weldable base + upper clip + rubber nose + high-strength bolt), the nose is the elastomer vulcanized onto the front of the clip toe, bearing directly down on the rail foot slant. English technical literature often calls it a rubber nose or elastomer nose. While rubber is a conventional name, actual materials span NBR, CR, EPDM, HNBR, as well as non-rubber elastomers like PU, TPU, and EVA. Related: FORGESAIL Bolted Rail Clip Products
AIST TR-13 defines the functional requirements that shape the role of the rubber nose: the clip must allow longitudinal float of the rail relative to the girder flange, restrict lateral movement strictly within 1/4 inch (tightened to 1/32 inch when using elastic rail pads), and provide continuous vertical pre-load via an elastomer to prevent rail pad creep. AISC further notes in its journal papers that applying vertical pre-load and lateral restraint via elastomers is the only method to satisfy the contradictory requirements of longitudinal float and lateral locking simultaneously. Rigid clips cannot achieve both, because longitudinal movement requires clearance, while clearance leads to lateral impact. Also read: Crane Rail Alignment Tolerance Guide

| # | Core Function | Engineering Meaning |
| ① | Apply constant vertical pre-load | Clamps edge seals of the under-rail pad, preventing ingress of water, mud, and dust under the rail. |
| ② | Absorb bow wave uplift displacement | Uses its own compressive deflection to “consume” uplift displacement, preventing alternating tensile forces from transmitting directly to the bolts. |
| ③ | Isolate steel-on-steel direct contact | Eliminates fretting corrosion between rail foot and clip toe, preventing fretting-induced rust. |
| ④ | Compensate for manufacturing & installation tolerances | Absorbs rail foot irregularities, clip height variances, and pad thickness tolerances. |
3. With vs. Without Rubber Nose: Why Noses Are Dominant Market Standard
3.1 Industry Consensus Verdict
Prior to the 1970s, crane rails widely relied on steel-on-steel rigid clips or J-bolts to hard-lock rails onto steel girders. This practice caused three well-acknowledged severe issues: extreme stress concentration, rapid wear of top girder flanges, and fatigue fracture of bolts under high-frequency alternating tensile stress. These challenges drove a global shift in crane engineering from “rigid fixing” to “elastic restraint”.
AIST TR-13 (2021 Edition) highlights the physical contradiction rigid solutions cannot resolve: clips must allow longitudinal thermal float while maintaining lateral restraint (movement ≤ 1/4″, or ≤ 1/32″ with pads). Achieving longitudinal float with zero lateral clearance via rigid steel clips is physically contradictory: sliding requires clearance, but clearance causes lateral impact. Rubber noses reconcile this via elastic deformation: vertical elasticity + low-friction longitudinal sliding + rigid lateral stopping. AISC succinctly comments: “The twisting-camming action in single-bolt clips caused by longitudinal creep continually pushes the rail off alignment.”
In China, GB 50278-2010 (Code for Construction and Acceptance of Lifting Equipment Installation Engineering) and National Standard Atlases 17G325 / 23G525 specify elastic pads and rubber noses as standard configurations rather than optional additions. Flexible clips with rubber noses are now the de facto standard globally.
3.2 11-Dimensional Technical Comparison
| Comparison Dimension | Noseless / Steel-on-Steel Rigid | Nosed / Flexible Clip | Conclusion |
| Uplift Path | Bow wave uplift forces go straight to bolts, causing high-amplitude alternating tensile stress. | Nose compression absorbs displacement; dynamic bolt stress amplitude drops significantly. | ✅ Nosed |
| Bolt Loosening | High failure rate: nut loosening → clip displacement → rail gnawing. | Elastic pre-tightening + self-locking wedge; loosening probability drops dramatically. | ✅ Nosed |
| Girder Fatigue | Point contact, stress concentration, high risk of top flange wear and fatigue cracking. | Works with pad to distribute loads evenly along rail base. | ✅ Nosed |
| Fretting Corrosion | Direct steel-steel friction, leading to severe rail foot fretting corrosion. | Elastic isolation layer eliminates metal-on-metal friction. | ✅ Nosed |
| Thermal Expansion | High longitudinal creep in long welded rails; rigid clips seize or wear out. | Allows longitudinal creep; essential prerequisite for long welded rails. | ✅ Nosed |
| Noise & Vibration | Metal impact noise; noticeable structural sound transmission. | Flexible system reduces noise by ~10 dB(A) and vibration up to 48%. | ✅ Nosed |
| Tolerance Compensation | Relies on high-precision machining and site shims. | Elastomer absorbs rail base roughness; lateral adjustability of 15–20 mm. | ✅ Nosed |
| Initial Cost | Simple structure, low unit price. | Requires vulcanization + matching pad, higher unit price. | ⚠️ Noseless |
| Extreme Temp Resistance | Unaffected by temperature. | Standard elastomers ~ −25 to +100 °C; high temp requires special formulas. | ⚠️ Noseless |
| Lifespan Weak Link | Weak link lies in bolts and girders (inspectable/tightenable). | Weak link shifts to the rubber nose (aging, wear, detachment). | Trade-offs exist |
| Wearing Part Replacement | No elastic wear parts. | Nose vulcanized to clip toe; traditionally cannot be replaced independently. | ⚠️ Noseless |


Key Insight: Flexible clips win in 7 of 11 engineering dimensions. Noseless rigid contacts still make sense in specific extreme conditions, such as non-resilient steel-on-steel fastening for extreme temperatures, very short rail segments, or legacy interfaces. Fully resolving this trade-off requires addressing two questions:
- How to boost nose stability and lifespan in harsh environments?
- Is there a more convenient maintenance method for replacing rubber noses?
4. An Overlooked Trade-Off: How Long Does a Rubber Nose Really Last?
Nose lifespan depends on four factors: installation process, intrinsic material aging, operating conditions, and interface quality.
4.1 Four Key Dimensions Determining Lifespan
① Initial Compression Allowance during Installation — The Underestimated Priority
This parameter is determined purely during installation, yet it directly dictates the lifespan of both nose and pad. Elastomers must be compressed to their designed initial pre-load upon installation. Also read: Heavy-Duty Crane Rail Installation Guide
- Over-compression: Minor rail height variations transfer uplift force straight to bolts, accelerating fatigue.
- Under-compression: Edge seals fail, allowing slurry and mud ingress that accelerates pad deterioration. Related: FORGESAIL Elastic Rail Pads
② Intrinsic Material Aging
Common Rubber Nose Materials: Selection & Applications
| Material | Advantages | Drawbacks | Applicable Scenarios |
| NBR (Nitrile) | Oil-resistant, wear-resistant, high cost-performance ratio (Mainstream) | Poor ozone/weathering resistance; prone to outdoor cracking | Indoor workshops, oily environments, metallurgical plants |
| CR (Neoprene) | Weather/ozone resistant, good adhesion to metal | Prone to hardening at low temperatures | Outdoor ports, coastal trestles |
| EPDM | Outstanding weather, ozone, and steam resistance | Relatively poor oil resistance | Most ports, outdoor/high-humidity conditions |
| PU (Polyurethane) | High wear/tear resistance, exceptional load capacity | Prone to hydrolysis; sensitive to damp heat | Dry, high-wear, heavy-load environments |
| EVA | Low cost, good damping, low-temperature flexibility | High creep; toe load decays noticeably over time | Light-load damping scenarios |
③ Operating Conditions
Duty cycles (A5, A6, A7) shift cyclic fatigue loads by an order of magnitude. High-frequency equipment like grab cranes and unloading bridges faces harsh environments. Longitudinal creep friction from thermal expansion and lateral shear from rail gnawing are silent killers. Also read: Rail Specifications & Standards Guide
④ Interface (Bonding) Quality: Determining “Worn Out” vs. “Fallen Off”
Approximately 70% of rubber-to-metal bonding failures are caused by inadequate metal surface treatment: zinc plating layer treatment, oxidation after sandblasting, uncalibrated vulcanization parameters, etc. With the same formula and the same drawing, the lifespan of rubber noses from different factories can be completely different. This is a process capability issue. (based on industry-wide failure analysis studies)

5. Forgesail’s Solution Tiers: From Reliability to Replaceable Architectures
Forgesail addresses rubber nose failures through three progressive tiers: stronger mainstream reliability, in-house customization for special working conditions, and a wrap-around replaceable architecture.
5.1 Tier 1: Optimized Design, Materials, and Process to Ensure the Overall Quality of Mainstream Products
Most failures of traditional rubber noses do not occur suddenly during operation. They are influenced by decisions made during installation and manufacturing. Forgesail exercises systematic control over four areas:
5.1.1 Precision Selection for Accurate Pre-Compression
According to the rail type, wheel load, work level and on-site foundation conditions, the rubber nose height and pre-compression are determined through a mature rail selection system. The pre-compression is the first threshold for the full life cycle performance of the rubber nose: if it is too large, slight rail height changes will directly transmit the uplift force to the bolt; if it is too small, the edge seal of the pad will not be tight, and mud and water intrusion will accelerate the deterioration of the pad.

Forgesail Clip Selection System: Matching Rubber Nose Height Based on Rail Profile and Duty Conditions Related: FORGESAIL Rail Clip Selection & Products
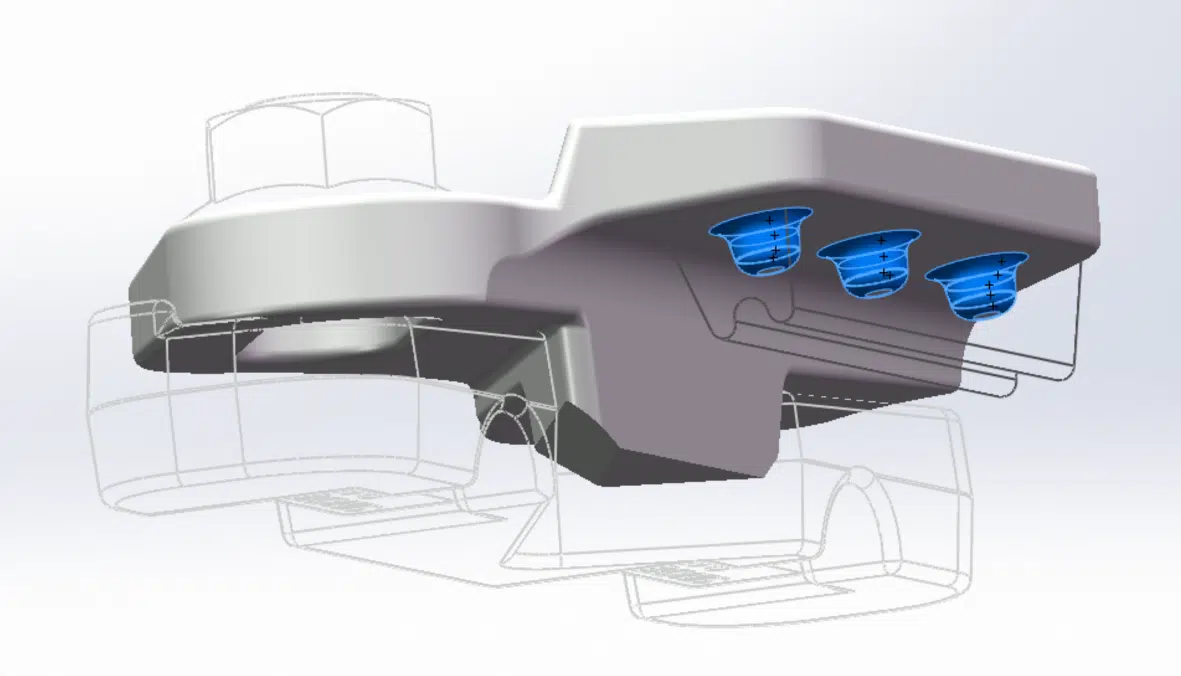
Studded Anchorage for Enhanced Mechanical Retention
Besides chemical bonding, mechanical interlocking is provided between the rubber nose and the clip body, so even with local aging the nose will not come off completely right away, buying time for scheduled maintenance. Related: FORGESAIL Crane Rail Clips
5.1.3 Premium EPDM Formulations to Extend Material Life
With high-quality EPDM as the main base material, combined with an ozone-resistant and aging-resistant additive system, the durability of the material is improved for open-air ports, coastal salt spray and high humidity conditions.
Laser De-Zincing, Specialized Adhesive, and Thermal Vulcanization to Improve Interface Strength
Before bonding, a laser removes the zinc layer from the clip surface so the zinc layer cannot become a weak bonding surface. A specialized adhesive system and thermal vulcanization then form a stable chemical bond between the elastomer and the metal, reducing bonding failure risk at the process source.
5.2 Tier 2: In-House Manufacturing Supporting Noseless Customization
The steel-to-steel rigid solution is outdated for the vast majority of heavy-load, high-frequency, long welded rail applications, but it still has niche value under extreme temperatures, spatial constraints, legacy interfaces, or special process requirements. Forgesail has its own factory in China and can customize noseless rail clips according to customer working conditions. Related: FORGESAIL Custom Rail Clip Solutions

5.3 Tier 3: Encapsulated Replaceable Nose — Architectural Resolution to Lifespan Mismatch
Forgesail has engineered a low-cost replaceable nose solution and filed corresponding patent applications. The wrap-around (encapsulated) Replaceable Nose Rail Clip turns the nose from a disposable component into a standardized consumable wearing part. It responds to four industry bottlenecks at once:
| Challenges | Current Status of Traditional Solutions | Forgesail’s Solutions |
| Lifespan Mismatch | The lifespan of the nose is usually only 1/3~1/5 of that of the steel body, but it cannot be individually replaced. | Matched Component Life: Steel body lasts full lifecycle; nose is replaced periodically. |
| Failure Predictability | Interface corrosion is gradual. The appearance can look normal, then the nose falls off as a whole. | Encapsulation + mechanical interlock: eliminating sudden complete detachment. |
| Replacement = Overall Scrap | Rubber nose end of life = forged steel pressure head + anti-corrosion coating + bolts are scrapped together | The nose is the only replaceable part; the steel body and mounting interface remain fixed. |
| Process constraints dictate material selection | Material selection prioritizes rubber compounds that are easiest to vulcanize to steel. | With mechanical interlocking as a fail-safe, NBR/CR/EPDM/PU/EVA can be selected based on the working conditions. |
Pillar 1: Adhesion, Shifting Failure Mode from Peel to Tear
This is the most compelling technical justification for the wrap-around (encapsulated) design.
A fundamental principle of material mechanics dictates that for any given elastomer, peel strength is significantly lower than its intrinsic tear strength. Traditional bonded rubber noses leave a free peel initiation edge that channels failure along the lowest-energy peel path; adhesive quality is usually not the limiting factor.
The wrap-around structure changes the force path. By forming the elastomer into a closed-loop encapsulation around the press head tip, integrated with dovetail grooves, undercuts, and through-hole interlocking features, it achieves three changes:
- Elimination of peel initiation points: With no free edge available for lifting, the pull-out load is shared between the hoop tension of the closed ring and the mechanical interlock. To dislodge the rubber nose, the elastomer body itself must first tear. This raises the failure threshold by an order of magnitude.
- Interface failure does not equal nose failure: Even if coastal salt spray or environmental corrosion degrades the local adhesive interface, the geometric interlocking still anchors the rubber nose to the clip head. This prevents the most dangerous failure scenario: sudden, complete detachment after prolonged service with no visible warning signs.
- Reduced dependence on process consistency: Roughly 70% of adhesive failures originate from fluctuations in surface preparation. The wrap-around geometry absorbs part of this risk through mechanical constraints and improves batch-to-batch stability without relying solely on process control.

Pillar 2: Replaceability, Redefining the Rubber Nose as a Standard Consumable
Replaceability is more than a convenience. It is the architectural change that directly addresses lifespan mismatch.
When the rubber nose becomes a replaceable standard consumable, several maintenance and lifecycle benefits follow:
| Aspect | Conventional Integrated Architecture | Forgesail Replaceable Nose |
| Service Life Matching | System lifespan is capped by the shortest-lived component. | Steel body serves the full lifecycle; the rubber nose is replaced on a scheduled cycle. |
| Maintenance Operations | Entire unit must be disassembled and replaced, often requiring rail realignment. | Loosen bolts, extract old rubber nose, insert new rubber nose, tighten. Rail remains in position. |
| Spare Parts and Logistics | Requires stocking complete forged steel assemblies – heavy, space-consuming, and costly to ship | Only replacement nose strips need to be stocked: lightweight and compact, with significantly lower logistics costs. |
| Application Adaptability | One material fits all | Same forged steel body + graded rubber nose, materials selected as needed |
| Aftermarket Penetration | Cannot retrofit into existing rail systems from other suppliers. | If the interface is compatible with mainstream models, direct entry into the replacement and retrofit aftermarket is feasible. |
| Circular Economy / ESG | Steel is scrapped together with the elastomer | Steel body is reused; carbon footprint and waste reduction data can be provided to customers. |
The Tier 3 replaceable nose design is now available as a standard product. See our replaceable nose rail clips for specifications, dimensions, and ordering information.
5.4 The Three-Tier Strategy: A Progressive Framework, Not a Menu of Options
The three tiers form a progression. Each layer addresses part of the same core challenge:
- Tier 1 secures material selection, adhesion, and service life for reliable performance under intended operating conditions.
- Tier 2 enables tailored material choices for exceptional or demanding service environments.
- Tier 3 resolves post-failure scenarios through a replaceable architecture that turns replacement into a scheduled task.
For most standard applications, this approach improves product consistency and reliability. For high-frequency duty cycles, aggressive coastal corrosion exposure, and long-span EPC projects, the encapsulated replaceable rubber nose supports lower lifecycle cost.
6. Frequently Asked Questions (FAQ)
Q1: What is the maintenance cycle for Forgesail clips?
A: It depends on duty frequency and environment. High-frequency port terminals (over 500,000 cycles/year) should be inspected every 2-3 years; standard industrial tracks every 5-8 years. Replacement thresholds: rubber permanent compressive set over 30%, or surface crack depth over 2 mm. Wrap-around (encapsulated) replaceable noses do not require rail realignment during replacement, reducing downtime. Related: FORGESAIL Port Crane Rail Solutions
Q2: Can Forgesail clips replace our existing rail fastener systems?
A: In most cases, installation dimensions and lateral adjustability allow 1:1 replacement with mainstream steel sole plates without structural modifications. Submit rail types and photos of current fasteners to the engineering team for confirmation. Related: FORGESAIL Crane Rail Sole Plates
Q3: Is a replaceable nose more prone to loosening or lower strength than vulcanized noses?
A: No. The wrap-around (encapsulated) nose employs dual anchoring (mechanical interlocking + chemical bonding). Pull-off and lateral load capacities meet or exceed traditional vulcanized products, as verified by type test reports. FORGESAIL’s production version is available here: replaceable nose rail clips
Q4: Does Forgesail support custom production?
A: Yes. With in-house factories in China, Forgesail custom-manufactures clips for specific industrial applications, including noseless options for rare conditions.
Q5: Are special tools or long downtime required to replace noses?
A: No. The wrap-around design requires only loosening bolts, sliding out the old nose, inserting the new nose, and re-tightening. Rail and baseplates stay fixed in position.
Q6: How does the replaceable nose affect total cost of ownership?
A: The initial unit price is comparable to premium vulcanized clips. Life-cycle savings come from three channels: eliminating whole-assembly scrapping when only the elastomer is worn, reducing crane downtime because no rail realignment is needed, and lowering spare parts inventory volume and shipping weight. For high-frequency port terminals and long-span EPC projects, accumulated savings typically offset the initial investment within the first replacement cycle.
7. Conclusion
The rubber nose is a structural functional component that withstands cyclic uplift forces. It is the key enabler that makes flexible rail clips the de facto standard in heavy-load, high-frequency, long welded rail applications.
Industry experience still shows the trade-off: a rubber nose has a limited service life, and conventional architectures cannot replace it independently. Forgesail’s approach does not rely on a single fix. It combines three tiers: improved mainstream reliability, in-house customization, and an encapsulated replaceable architecture that turns what happens when the rubber nose fails into a planned maintenance action.Engineers get matched preload during selection. Procurement and plant owners stock lightweight replacement nose strips instead of completeforged steel assemblies. Long-lifecycle projects keep the steel body and replace only the elastomer. The inability to replace the nose was the weak link, not the rubber itself. Changing the architecture makes crane rail fasteners maintainable.
If you are planning a new project or evaluating retrofit options for existing rail systems, contact the Forgesail Engineering Team. We can provide tailored solutions based on rail profile, duty class, and site-specific conditions. You can submit your rail profile and duty class for a tailored clip recommendation, download the product catalog for detailed specifications, or request sample clips for on-site compatibility testing. For projects requiring replaceable nose architecture, see FORGESAIL’s replaceable nose rail clip product page for full specifications and technical drawings.
References
This document is prepared based on the following authoritative technical references and the project experience of the Forgesail Engineering Team:
- AIST TR-13 – Guide for the Design and Construction of Mill Buildings (2021), Association for Iron & Steel Technology.
- AISC – New Fatigue Provisions for the Design of Crane Runway Girders, American Institute of Steel Construction.
- GB 50278-2010 – Code for Construction and Acceptance of Lifting Equipment Installation Engineering (China).
- GB/T 3811 – Design Code for Cranes (China).
- National Standard Design Drawings 17G325 / 23G525 – China national building standard design diagrams.
- Domestic engineering literature, including but not limited to: “Improvement of Rail Clamps for General-Purpose Bridge Cranes” and other relevant Chinese technical publications.
The mechanical principle of the bow wave is derived from the fundamental theory of beams on elastic foundations, a well-established body of knowledge in structural mechanics (Hetényi, 1946).