Thermite welding crane rail is the most effective solution to eliminate split bolted joints for heavy-duty overhead and gantry crane runway. Every bolted rail joint is a potential failure point. In heavy-duty crane applications — shipyard gantry cranes, port container cranes, steel mill ladle cranes — a single loose fishplate can cascade into rail misalignment, accelerated wheel wear, and unplanned downtime costing thousands per hour.
Aluminothermic (thermite) welding eliminates the joint entirely. The result is a continuous, seamless rail with mechanical properties matching the parent rail. For track end protection, see our crane rail buffer stops — no bolts to loosen, no gaps to hammer, no step to form.
This guide covers the complete thermite welding process for crane rails, the products and equipment involved, applicable rail profiles, and field-proven best practices.
1. What Is Aluminothermic Welding?
Aluminothermic welding uses a chemical reaction between aluminum powder and iron oxide to produce molten steel at approximately 2,500°C in under 30 seconds. When poured into a refractory mold surrounding the rail ends, the superheated steel fuses the rail ends together into a single continuous structure.
The Chemical Reaction
The core reaction is:
Fe₂O₃ + 2Al → 2Fe + Al₂O₃ + heat (≈3,500 kJ)
In the chemical reaction of thermite welding crane rail, the aluminum reduces the iron oxide, producing pure molten iron and aluminum oxide slag. The slag, being lighter, floats to the top while the molten steel fills the weld cavity around the rail ends for thermite welding crane rail.

Why It’s Superior to Bolted Joints
| Property | Bolted Fishplate Joint | Aluminothermic Weld |
| Electrical continuity | Variable, degrades over time | Equal to parent rail |
| Mechanical strength | ~60-70% of parent rail | ≥100% of parent rail (tensile) |
| Maintenance requirement | Periodic bolt re-torquing | None |
| Impact loading | Wheel impact at every joint | No impact — continuous surface |
| Service life | 2-5 years (heavy duty) | 20+ years |
| Fatigue resistance | Low — bolt hole stress concentration | High — no stress risers |
2. Supported Rail Profiles for Thermite Welding Crane Rail
Forgesail’s thermite welding consumables cover the full range of crane rail profiles in common use worldwide:
Chinese GB Standard (QU Series)
| Rail Profile | Thermite Portion (kg) | Preheat Time (min) | Applications |
| QU70 | 4.0 | 3 | Medium duty overhead cranes, workshop cranes |
| QU80 | 4.5 | 4 | Heavy workshop cranes, warehouse cranes |
| QU100 | 9.0 | 5 | Heavy gantry cranes, port RTG cranes |
| QU120 | 12.0 | 9 | Shipyard Goliath cranes, heavy portal cranes |

European DIN 536 A-Series
| Rail Profile | Thermite Portion (kg) | Preheat Time (min) | Applications |
| A55 | 4.0 | 3 | Light overhead cranes |
| A65 | 4.5 | 4 | Medium factory cranes |
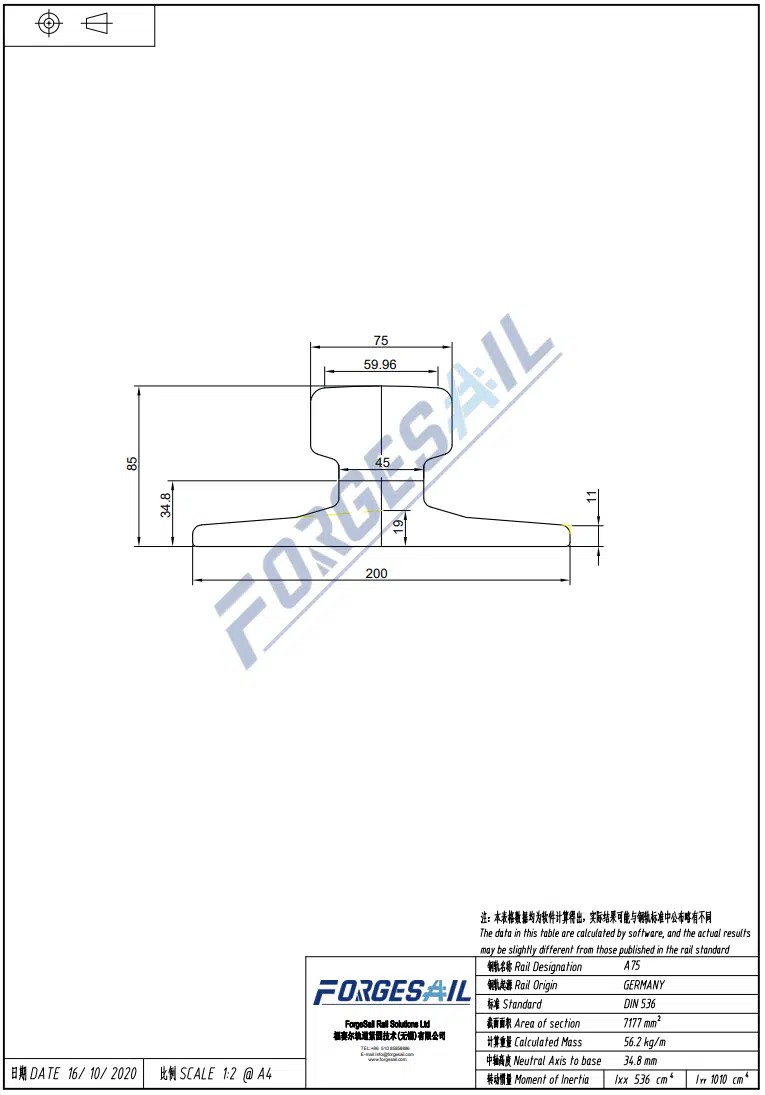
| A75 | 5.0 | 5 | Heavy workshop cranes |
| A100 | 9.0 | 9 | Container terminal cranes |
| A120 | 12.0 | 12 | Heavy gantry cranes |
| A150 | 15.0 | 15 | Ultra-heavy shipyard Goliath cranes |
Other Supported Rail Types
– 50 kg/m and 60 kg/m railway rails
– 18 kg/m, 24 kg/m, 38 kg/m, 43 kg/m light rails
– Custom rail profiles available on request
3. Standard Operation Steps of Thermite Welding Crane Rail
Step 1: Inspect and Clean Rail Ends
Remove all rust, scale, oil, and moisture from the rail ends. Any contamination will cause porosity in the weld. The rail ends must be cut square — if they’re worn or angled, re-cut before proceeding.
Step 2: Align Rail Ends
Position rails with the specified gap (26 ± 2 mm for all Forgesail thermite portions). Use the rail alignment device to ensure:
– Vertical alignment: both rail heads at exactly the same height
– Horizontal alignment: rail centerlines perfectly in line
– No twist or tilt
Misalignment at this stage becomes a permanent defect in the finished weld.
Step 3: Place the Sand Mold
The two-piece refractory sand mold surrounds the rail ends, forming the weld cavity. Center the mold precisely over the rail gap. The mold cavity shape is pre-engineered to produce a weld collar that can be ground flush.

Step 4: Apply Luting Sand
Seal all mold-to-rail interfaces with luting sand (refractory paste). Any gap will leak molten steel during pouring. Pay special attention to the rail foot — this is where leaks most commonly occur.
Step 5: Check Welding Materials
Verify:
– Thermite portion is the correct type for the rail profile
– Portion is dry (moisture causes violent spatter during reaction)
– Crucible is clean with no cracks
– All tools (dross blade, crucible cover, slag tray) are ready
Step 6: Preheat
Use the propane/oxygen preheater to heat the rail ends. Key parameters:
| Parameter | Value |
| Oxygen pressure | 0.4 MPa |
| LPG pressure | 0.07 MPa |
| Flame core length | 15-20 mm |
| Oxygen flow rate | 3,500 L/h |
| Preheat time | 3-15 min (varies by rail size, see tables above) |
The preheat is critical — it drives moisture out of the mold, brings the rail ends to welding temperature, and ensures the molten steel flows completely into the rail foot before solidifying. Proper preheating is essential to guarantee qualified thermite welding crane rail construction.

Step 7: Pouring
1. Place the thermite portion into the preheated crucible
2. Ignite using a spark igniter (never a flame — it can cause splash)
3. The reaction completes in approximately 15-30 seconds
4. Immediately tap the crucible to release the molten steel into the mold
5. Allow 1-2 minutes for solidification
The slag (aluminum oxide) floats to the top of the riser and is discarded after the pour.
Step 8: Demount Mold and Remove Dross
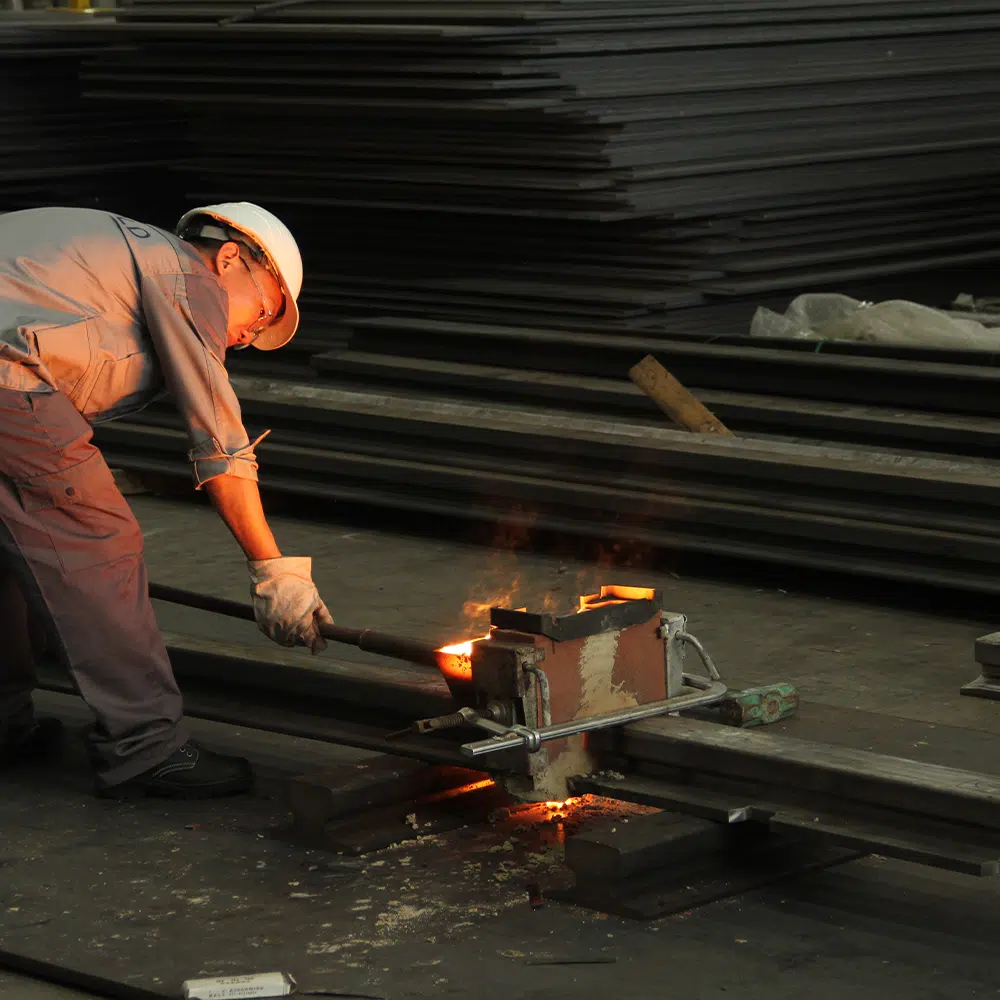
After 4-5 minutes of cooling for thermite welding crane rail, break away the sand mold. Use the dross blade to remove the top riser while the metal is still hot (red heat). The riser contains slag and shrinkage porosity and must be fully removed to ensure qualified thermite welding crane rail finish.
Step 9: Grinding
Once cooled to ambient temperature, grind the weld collar flush with the rail head profile. The finished surface must be:
– Flush with surrounding rail surface (no step)
– Smooth — no gouges or grinding marks deeper than 0.3 mm
– Blended smoothly into the rail head radius

Step 10: Testing (MPI / UT)
Quality verification:
– Magnetic Particle Inspection (MPI): Detects surface and near-surface defects
– Ultrasonic Testing (UT): Detects internal porosity, lack of fusion, and cracks
– Visual inspection: Check for undercut, overlap, grinding marks

4. Welding Parameters Summary
All Forgesail thermite portions use the same baseline parameters:
| Parameter | Specification |
| Oxygen pressure | 0.4 MPa |
| LPG pressure | 0.07 MPa |
| Flame core length | 15-20 mm (neutral flame) |
| Oxygen flow rate | 3,500 L/h |
| Reserved rail gap | 26 ± 2 mm |
| Reaction time | 15-30 seconds |
| Pour temperature | ~2,500°C |
| Weld tensile strength | ≥680 MPa (III DE series) |
| Applicable standard | TB/T1632.3-2014 |
| Quality system | ISO 9001:2008 |
5. Cold Weather Precautions
Aluminothermic welding below 15°C requires additional steps to prevent cold cracking:
| Condition | Procedure |
| Air temperature below 15°C | Cover the weld head with an insulating blanket for 10 minutes after pouring |
| Rail temperature below 15°C | Use a welding torch to preheat each rail side for 1-2 minutes until reaching approximately 37°C |
| Wet or humid conditions | Extended preheat to drive moisture from mold and rail surface |
| Windy conditions | Use wind shields around the welding area to prevent uneven cooling |
6. Complete Welding Kit Contents
A Forgesail aluminothermic welding kit includes everything needed for field welding:
| Component | Function |
| Thermite portion (III DE / QU series) | Provides molten steel for the weld |
| Two-piece sand mold | Forms weld cavity around rail ends |
| Crucible | Contains the thermite reaction |
| Crucible cover | Controls reaction and prevents splash |
| Slag receiving hopper | Catches slag after pour |
| Preheater with rack | Propane/oxygen preheat system |
| Propane pressure reducer | Regulates LPG flow |
| Rail alignment device | Positions rails for welding |
| Rail grinder | Post-weld finishing |
| Bow clamp | Secures mold during pour |
| Dross blade | Removes riser after welding |
| Luting sand | Seals mold-to-rail interface |

All equipment is portable and requires no external power source — the chemical reaction is self-sustaining.
7. Applications Across Industries
Aluminothermic welding has been widely adopted for crane rail applications across multiple industries:
| Industry | Application | Benefit |
| **Ports & Terminals** | STS and RTG crane rails | Zero joint impact allows high-speed trolley travel |
| **Shipyards** | Goliath gantry crane runways | Continuous rail eliminates joint failure under extreme loads |
| **Steel Mills** | Overhead ladle crane tracks | Welded joints handle thermal cycling without loosening |
| **Automated Warehouses** | ASRS stacker crane rails | Seamless joints enable precise positioning at 200+ m/min |
| **Mining** | Stacker/reclaimer rails | Welded joints resist heavy impact and abrasive environments |
| **Coking Plants** | Quenching car rails | Continuous rails handle thermal shock without joint degradation |
| **Railway Freight Yards** | Gantry crane rails | Eliminates bolted joint maintenance in high-traffic areas |
8. Quality and Compliance
Forgesail’s III DE series thermite portions for thermite welding crane rail have been tested and certified by authorized quality inspection authorities to meet TB/T1632.3-2014, the Chinese national standard for aluminothermic welding. All supporting equipment for thermite welding crane rail conforms to ISO 9001:2008 quality management system requirements.
Each thermite portion is individually sealed and packaged to prevent moisture absorption during storage and transport.
9. Common Weld Defects and Prevention
| Defect | Cause | Prevention |
| **Porosity** | Moisture in mold or rail surface | Adequate preheat; store portions in dry conditions |
| **Lack of fusion** | Insufficient preheat; rail too cold | Verify preheat time; heat cold rails before welding |
| **Slag inclusion** | Incomplete dross removal; contaminated portion | Clean dross blade; use sealed portions |
| **Hot cracking** | Rapid cooling; high restraint | Insulating blanket in cold weather; correct rail gap |
| **Surface pitting** | Grinding too aggressively | Use proper grinding wheel; let weld cool fully |
10. Why Choose Forgesail Thermite Welding Products
Complete system: Forgesail supplies not just the thermite portion, but the entire welding kit — molds, crucibles, tools, preheaters, grinders, and alignment devices. One supplier, one standard, one point of contact.
Broad rail compatibility: From QU70 light crane rails to A150 heavy Goliath crane rails, Forgesail stocks matching consumables for thermite welding crane rail and supplies thermite portions for the full range. Custom formulations available for non-standard profiles of thermite welding crane rail.
Proven quality: All III DE series portions are certified to TB/T1632.3-2014. ISO 9001:2008 manufacturing ensures batch-to-batch consistency.
Global support: Engineering team available for on-site training, procedure qualification, and troubleshooting. Manufacturing facilities in Wuxi and Nantong, China, with export logistics worldwide.

Conclusion
Thermite welding crane rail uses aluminothermic welding to transform a crane rail joint from a maintenance liability into a permanent, seamless connection. For facilities operating heavy cranes — shipyards, ports, steel mills, mines, automated warehouses — thermite welding crane rail cuts downtime, extends rail life, and eliminates the recurring cost of bolted joint maintenance.
The welding process is field-portable, requires no external power, and can be performed by trained technicians in a single shift. With proper preheat, alignment, and post-weld testing, a thermite-welded joint will outlast the surrounding rail.
—
If you need supporting materials for thermite welding crane rail, contact our team for quotation.(https://forgesail.com/contact/) | Email: info@forgesail.com | Tel: +86-(0)510-85858896