




YB/T 5055 QU70 Crane Rail – Dimensions, Weight & Specifications
Also specified as: QU70 crane rail, YB/T 5055 QU70, QU70 rail (70 mm head), 52.8 kg/m crane rail.
- 70 mmHead width
- 120 mmHeight
- 120 mmBase width
- 52.8 kg/mWeight per metre
- 12 mStandard length
QU70 is the entry size of the GB crane rail range. A 70 mm head, 120 mm high section, 120 mm base, 52.8 kg per metre. It suits light overhead cranes and workshop tracks where the loads are modest and the rail has to be easy to handle.
One supplier from mill order to container. ForgeSail handles QU70 crane rail as a single supply: we source the rail, pre-machine it to your drawing, make the matching clips, sole plates, pads and fishplates, supply the aluminothermic welding consumables if the track will be welded, and pack the whole shipment to meet international transport rules. You deal with one order, one inspection and one bill of lading instead of chasing a mill, a machinist, a fastener supplier and a packer to finish before the vessel closes.
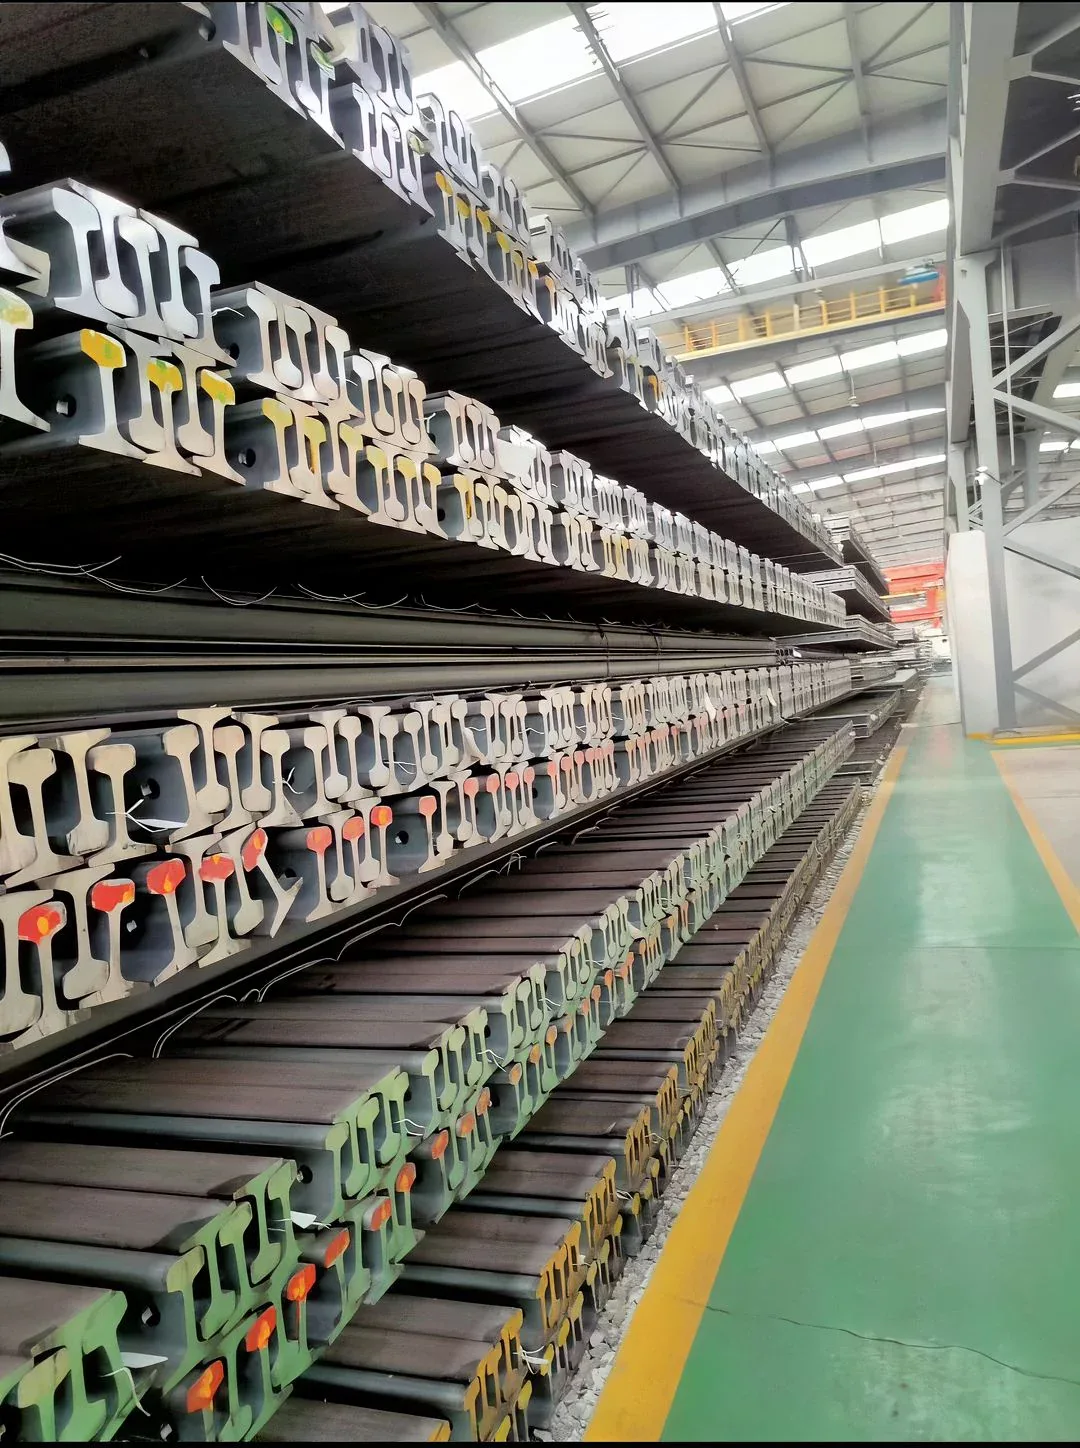
YB/T 5055 QU70 crane rail dimensions and weight
| Standard | YB/T 5055 (QU crane rail) |
|---|---|
| Profile | QU70 |
| Head width (C) | 70 mm |
| Height (A) | 120 mm |
| Base width (F) | 120 mm |
| Mass | 52.8 kg/m |
| Weight per 12 m bar | ≈ 633.6 kg |
| Steel grades | 900A, 1100 (European standard); U71Mn, U75V (Chinese standard); carbon steel to ASTM on request |
| Standard length | 12 m; custom lengths available on request |
| Processing | Precision cutting, 45° mitre cutting, web drilling, milling and bending in our own workshop |
| Quality documents | Original Mill Test Certificate (MTC) with every shipment; third-party inspection welcome |
| Drawing | YB/T 5055 QU70 crane rail section drawing (PDF) |
QU70 vs QU80: sizing a GB-standard runway
Both follow YB/T 5055 and share the same family geometry, so the clip and base plate arrangement is similar. QU70 carries a 70 mm head at 52.8 kg/m; QU80 carries an 80 mm head at 63.69 kg/m and stands 10 mm taller at 130 mm.
QU70 suits light workshop cranes and short spans. Move to QU80 when the crane gets heavier or the runway longer, and the extra head width starts to matter for wheel contact stress. Because both profiles are in the same standard family, staying inside QU makes a later upgrade easier than switching standards.
Rail fabrication: cutting, drilling and joint preparation
QU70 is rarely ready to lay as it comes off the mill. We machine it in our own workshop before it ships, so it reaches your site already matching the fastening layout on your drawing.
- Web drilled to your fishplate pattern or your own plate drawing, in standard joint-bar spacings or to a custom hole chart.
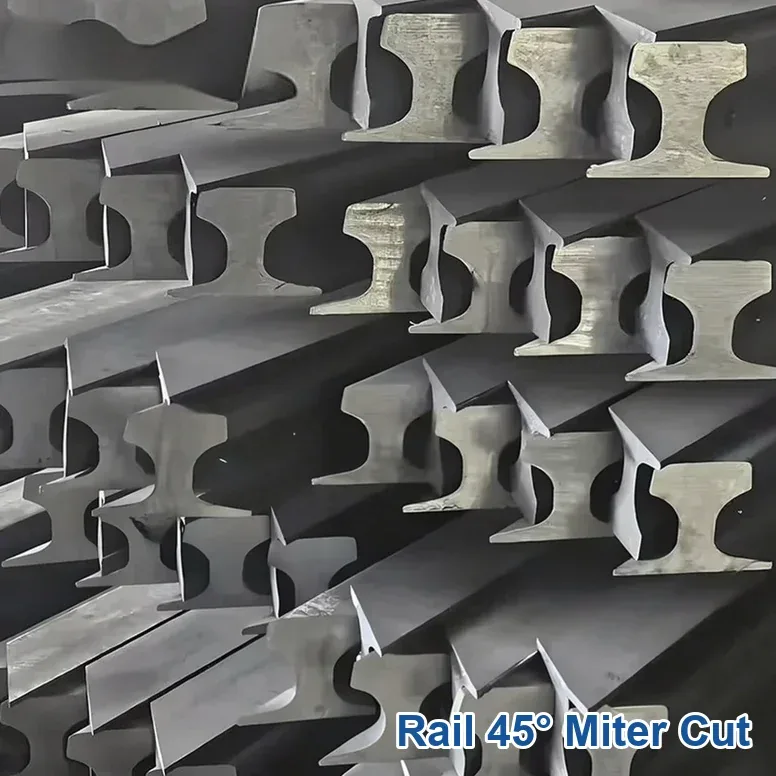
- Ends square cut or mitred at 45° where the track turns. Cut lengths follow your installation drawing rather than the nominal 12 m bar.
- Fishplates matched to the QU70 web and drilled to the same pattern, so a joint bolts up on site without rework.
- Aluminothermic welding kits with the mould, crucible and welding portion for the QU70 profile.
Why web drilling has to be accurate
On a bolted joint the drill pattern is the whole connection. Different rail standards use different hole diameters and spacings, so a hole that drifts out of position does not just slow the fitter down, it changes how the joint carries load.
| If this is wrong | What happens on site |
|---|---|
| Hole position | The fishplate bolt will not enter cleanly. Forcing it puts the bolt into eccentric load, which loosens the joint over time and can crack the bolt under repeated wheel impact. |
| Hole perpendicularity | A skewed hole makes the bolt sit at an angle. The nut and washer do not seat flat, torque is not transmitted evenly, and the bolt works loose under vibration. |
| Hole wall finish | A rough bore grips the bolt instead of letting it preload. The fitter reads high torque but the joint is not actually tight, and the bore becomes a fatigue origin. |
Welded or bolted joints: which one for your track
Every QU70 rail line has joints in it. You can bolt them with fishplates, or you can weld them out. The right answer depends on whether the rail ever has to come apart again, what the wheel loads are, and whether the track carries a signalling circuit.
When to bolt the joint with fishplates
A fishplate joint uses two joint bars bolted through the rail web, clamping the two ends together. It is the right choice when the joint has to stay openable: sections that will be lifted or replaced, insulated joints for track circuits, connections between two different profiles, temporary track, and expansion joints on bridges.
The trade-off is mechanical. A bolted fishplate joint carries roughly 60–70% of the parent rail's strength, and the bolt holes are stress risers. On heavy-duty crane track the fishplates are a wear item, typically replaced every 2 to 5 years, and the bolts need periodic re-torquing.
When to weld the joint
Welding removes the joint and gives you a continuous running surface. It suits fixed, long-run, high-load track where the rail will not need to come apart. Aluminothermic (thermite) welding is the field method: no power needed, light portable equipment, standard for repairs and for closing the gap between two welded strings on site. Flash butt welding is the electrical resistance method, normally done in a workshop where long strings are prefabricated before they ship.
How the three compare
| Bolted fishplate | Thermite weld | Flash butt weld | |
|---|---|---|---|
| Joint strength | 60–70% of parent rail | 90–96% of parent rail | 95–100% of parent rail |
| Fatigue resistance | Low, hole stress raisers | Good | Best, narrow heat-affected zone |
| Power needed | None | None | Yes, heavy generator or mains |
| Maintenance | Re-torque bolts periodically | None after welding | None after welding |
| Heavy-duty life | 2–5 years | Long | Longest |
| Can be taken apart | Yes | No | No |
Most projects use both. Rail is prefabricated in the workshop by flash butt welding into long strings, joined on site by thermite welding, and left with bolted fishplate joints at the insulated sections, bridge expansion joints and buffer rails.
Ask which joint suits your track
Matching fastening components for QU70
QU70 sits on rail clips and a base or sole plate, with a rubber pad under the rail where the design calls for one. We make all three, so the clips, plates and pads arrive as one matched set for your rail seat instead of three parts from three suppliers.
QU70 on light overhead cranes
QU70 is the smallest profile in the GB crane rail range and it suits installations where the crane is light and the span is short. Head width matters less at this end of the range because wheel loads are modest, so the deciding factors become handling weight and the availability of matching clips and base plates.
At 52.8 kg per metre a 12 m bar is about 634 kg, which most site cranes and small forklifts can handle without special rigging. If the crane is a standard workshop unit and the runway is under about 20 m, QU70 usually covers it. Longer spans or heavier wheels move you to QU80.
Export packing and container loading
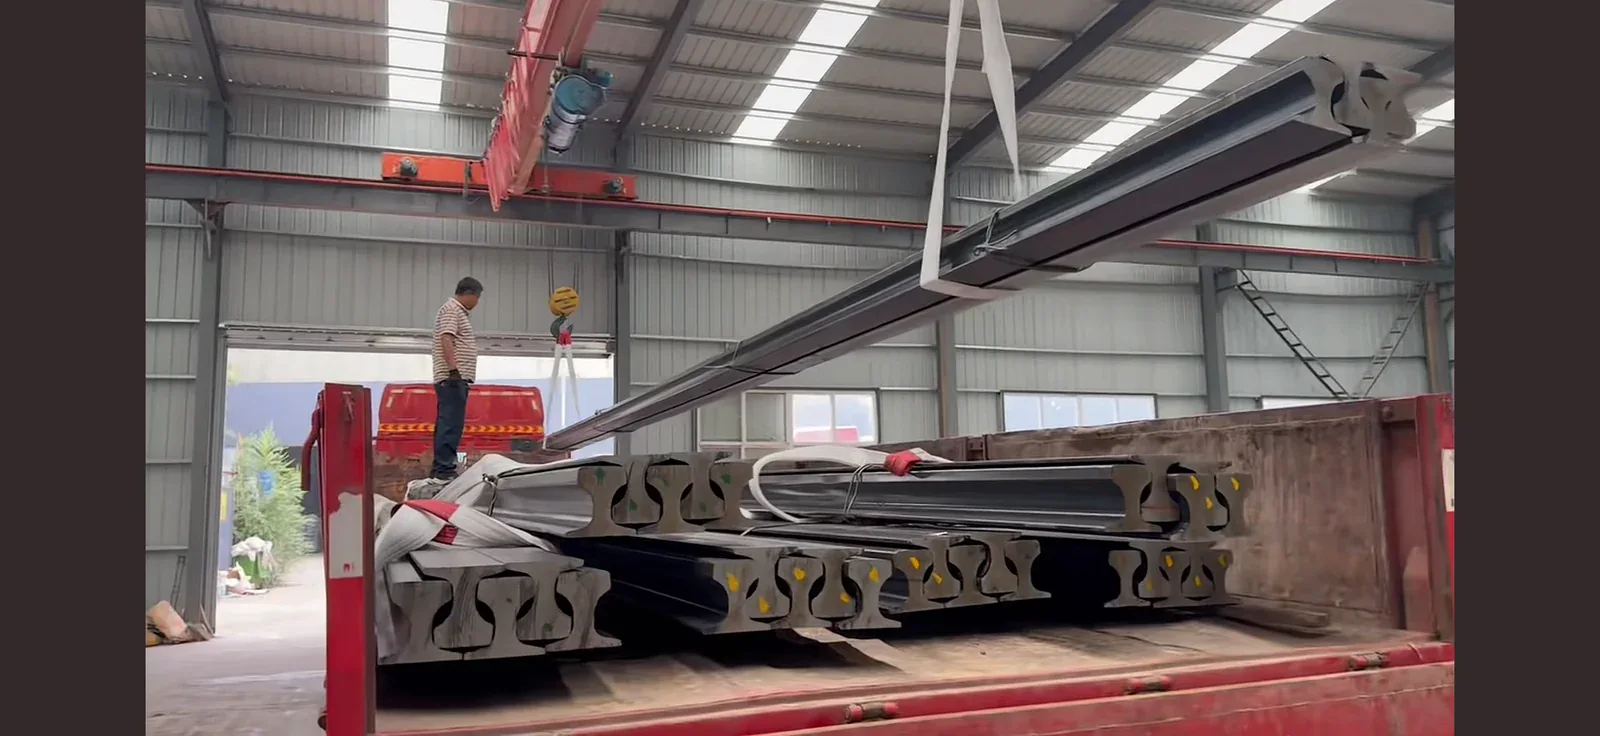
Rail leaves the workshop as a bundled, protected shipment, packed to meet the importing country's rules rather than handed over to the forwarder to sort out.
How the rail is bundled
- Surface protection goes on first, to limit rust during the sea voyage.
- Bars are tied into bundles with high-strength steel strapping, with wooden dunnage or spacers between the layers so the profiles do not rub.
- Each bundle is prepared for safe lifting, so the receiving yard can crane it out without damaged edges.
- Fastening components ship separately from the rail, in reinforced crates or cartons with moisture protection.
Does the packing need wooden dunnage?
Yes. The wooden dunnage between rail layers is not the same thing as a railway sleeper. It is a spacer and support, used to stop the bars rubbing and to spread lifting load across the bundle. Because it is wood crossing a border, it has to meet the importing country's ISPM 15 heat-treatment or fumigation rules.
Which container for QU70 rail
Crane rail usually ships either in a general-purpose container or as breakbulk, and the deciding factor is the cut length. QU70 is produced in 12 m standard lengths, so the container has to be long enough for the actual bar.
| Rail length | Container | Feasibility |
|---|---|---|
| 12 m (standard) | 40ft high cube | Normal option. The 40ft internal length is about 12.03 m, so a 12 m bar clears the doors with only a few centimetres to spare. |
| 10 m | 40ft standard | Comfortable fit with room left for blocking and lashing. |
| 6 m | 20ft standard | Does not fit. A 20ft box is about 5.90 m internally. |
| 5.8 m or shorter | 20ft standard | Fits cleanly. Suitable for short repair rails or workshop lengths. |
Where YB/T 5055 QU70 crane rail is used
- Light overhead cranes in the 5–30 t range
- Workshop and maintenance bay tracks
- Short-span runways where the rail weight has to stay manageable
- GB-standard projects that may step up to QU80 later
- Retrofit projects where the surrounding track stays on the same profile
- Mixed shipments where QU70 is one size in a larger rail order
Installation notes for YB/T 5055 QU70 crane rail
- QU70 is normally fixed with rail clips and sole plates. Welded and bolted clip systems both work, and the choice comes down to load capacity and whether the rail will ever have to be lifted again.
- The 120 mm base needs a continuous sole plate or base plate bed under it. Check that bed for flatness before the rail goes down.
- Where the design calls for a bolted joint, the rail arrives drilled to match the fishplates. Where it is to be welded, the ends are prepared for the welding method instead.
- Set gauge, straightness and elevation against the crane manufacturer's tolerance, then tighten the clips. Grouting under the base plate normally comes after the rail line is fixed.
Frequently asked questions about YB/T 5055 QU70
What is the difference between QU70 and the neighbouring sizes?
QU70 is one step in the YB/T 5055 QU section range: a 70 mm head, 120 mm height and 120 mm base at 52.8 kg/m, about 633.6 kg per 12 m bar. Adjacent sizes share the family geometry but change head width and mass, so they are not interchangeable on the same rail seat.
Which crane capacity is QU70 suitable for?
QU70 is typically specified for cranes in the 5–30 t class. The final choice depends on wheel load, wheel spacing, span and duty class rather than crane capacity alone. Send the crane data and our engineers will confirm the profile.
Which steel grades and lengths are available for QU70?
900A and 1100 (European standard), U71Mn and U75V (Chinese standard) and carbon steel to ASTM specifications. Standard length is 12 m; custom lengths and head-hardened options are available on request.
Can you supply QU70 rail cut, drilled and ready to install?
Yes. We source the QU70, cut and drill it in our own workshop, make the matching rail clips, sole plates, pads and fishplates, supply the aluminothermic welding consumables for welded track, and pack the shipment to export standards. Rails arrive drilled to your fishplate pattern and mitred where the track turns, with the fasteners in the same shipment. Every consignment includes an original Mill Test Certificate.
Can QU70 crane rail be shipped in a 20ft container?
Only if the bars are cut short enough. A 20ft container is about 5.90 m internally, so a standard 12 m bar will not fit. Full-length rail normally ships in a 40ft high cube or as breakbulk. For 20ft containers we cut to 5.8 m or shorter.
Does the rail need wooden dunnage for shipping?
Yes. The bundles use wooden dunnage between the rail layers to stop the profiles rubbing and to spread the load when the bundle is lifted. This is a shipping spacer, not a railway sleeper. Because it is wood crossing a border, it has to meet the destination country's ISPM 15 heat-treatment or fumigation rules, and we handle that as part of the export packing.
Should QU70 crane rail be bolted or welded?
It depends on whether the joint has to stay openable and how heavy the track is. Bolt with fishplates where the rail may need to be lifted or replaced, where an insulated joint is required for signalling, where two different profiles meet, or at bridge expansion joints and buffer rails. Weld it where the track is fixed, long and heavily loaded, using flash butt welding for workshop prefabrication and thermite welding for field joints and repairs.
Can I upgrade from QU70 to QU80 on the same track?
Not without changing the rail seat. Both follow YB/T 5055 and share family geometry, but QU80 has a wider head (80 mm against 70 mm), a taller section (130 mm against 120 mm) and a 130 mm base against 120 mm. The clip and base plate layout has to match the profile you fit.
